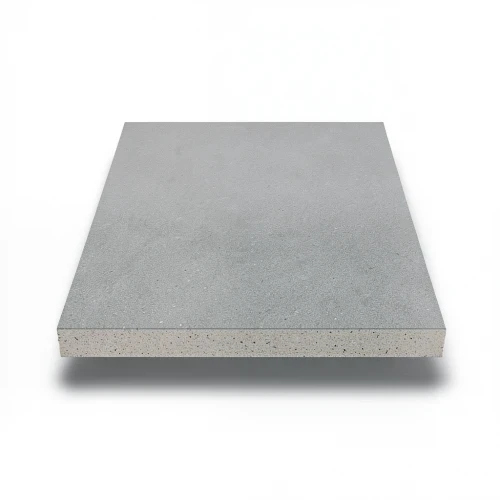
Mineral Composite Flooring System
(20 Product Views)
Durable, non-combustible mineral-based flooring solution ideal for high-traffic industrial and commercial spaces.
in stock
Product description
Mineral composite flooring is a high-performance surface solution engineered from inorganic mineral aggregates, cementitious binders, and specialized additives. Unlike organic flooring options, this system offers superior fire resistance, chemical stability, and structural integrity, making it a preferred choice for demanding environments where safety and longevity are paramount.
Key Features
- Non-Combustible: Provides an A1 fire rating, enhancing safety compliance in industrial facilities.
- High Load Bearing: Designed to withstand heavy foot traffic, forklifts, and industrial machinery without degradation.
- Chemical Resistance: Withstands spills from oils, solvents, and mild acids, ensuring long-term durability.
- Low Maintenance: The seamless, non-porous surface is easy to clean and resistant to staining.
Applications
This flooring system is widely used in manufacturing plants, warehouses, laboratories, hospitals, and commercial kitchens. Its seamless nature helps maintain hygiene standards, while its robust composition ensures a long service life with minimal repair costs.


